Explore our high-efficiency modular container units, prefabricated expandable structures, and integrated portable sanitation systems manufactured for worldwide deployment.
Analyzing the shift toward eco-conscious outdoor infrastructure, high-density polyethylene (HDPE) manufacturing standards, and non-sewer sanitation technology (NSST).
The global demand for high-efficiency mobile sanitation solutions has undergone a paradigm shift over the past decade. Historically categorized as rudimentary outdoor accessories, modern portable urinals and camping toilet systems are now recognized as vital modular infrastructure. Rapid expansion in outdoor eco-tourism, high-altitude commercial expeditions, large-scale disaster response operations, and off-grid construction sites has catalyzed rigorous engineering requirements for every tier-1 high-quality portable urinal camping supplier & suppliers worldwide.
According to current market intelligence, the global portable sanitation industry is rapidly expanding toward a multi-billion dollar valuation. Growth is predominantly propelled by strict environmental regulations regarding human waste management in pristine natural ecosystems, alongside heightened consumer standards for hygiene in luxury glamping and recreational vehicle (RV) travel. Procurement heads, commercial B2B buyers, and municipal logistics planners are no longer evaluating vendors solely on unit price; selection matrices now prioritize chemical resistance, fluid dynamics, structural durability, ergonomic portability, and environmental lifecycle impacts.
Implementation of UV-stabilized, high-molecular-weight polyethylene preventing odor absorption, structural cracking, and chemical degradation under extreme environmental conditions.
Integration of biological non-return silicone valve membranes and active mechanical vapor traps to ensure absolute odor containment without requiring continuous water flushes.
Engineered for high-density nestable transport, modular stackability in shipping containers, and rapid field assembly for emergency response and global supply chains.
How concentrated raw material ecosystems, automated blow-molding technologies, and lean manufacturing drive global value leadership.
China’s modular housing and sanitation equipment manufacturing hubs—particularly within Jiangxi, Zhejiang, and Guangdong industrial corridors—deliver unmatched economic efficiency. By consolidating tooling design, custom mold fabrication, resin compounding, and final assembly within localized 50-kilometer radii, top-tier Chinese manufacturers drastically collapse lead times.
Where Western OEMs often face fragmented component sourcing and high labor overheads, Chinese manufacturers leverage high-tonnage automated injection molding and multi-station blow-molding equipment capable of producing thousands of precision units per 24-hour shift cycle with sub-millimeter tolerances.
For international buyers requiring bespoke dimensions, integrated solar LED illumination, automated chemical dosing systems, or customized brand liveries, Chinese manufacturing hubs offer low Minimum Order Quantities (MOQs) for custom tooling. This agility enables global distributors to rapidly iterate product designs and respond to localized consumer trends without incurring prohibitive capital expenditure.
| Assessment Parameter | China Industrial Hubs | Traditional Overseas OEMs |
|---|---|---|
| Mold Tooling Lead Time | 15 – 25 Days | 60 – 90 Days |
| Raw Material Integration | Direct Resin Pipeline / On-site Compounding | Third-party International Sourcing |
| Container Loading Ratio | Nestable Engineering (Up to 1,200 units/40' HC) | Standard Packing (approx. 450 units/40' HC) |
| Production Scalability | 10,000+ Units / Week per Line | 1,500 – 3,000 Units / Week per Line |
| Certification Compliance | CE, REACH, ISO9001, ISO14001 Pre-verified | Variable per Sub-contractor |
From extreme mountain bivouacs to high-end glamping resorts and commercial construction zones.
High-end eco-resorts require luxury aesthetic integration paired with strict "Leave No Trace" zero-discharge waste containment. Modular urinals with sleek matte finishes and silent bio-deodorizing cartridges maintain guest satisfaction while upholding environmental compliance in pristine wilderness reserves.
Following natural disasters or humanitarian crises, immediate sanitation deployment is vital to prevent waterborne disease outbreaks. Lightweight, ultra-portable camping urinals and flat-pack container toilet blocks can be air-dropped or rapidly deployed by international aid agencies.
Remote mining sites, pipeline construction corridors, and telecom tower installation projects operate far from municipal sewer grids. Heavy-duty portable urinals with integrated waste-level indicators provide rugged, low-maintenance sanitation for multi-shift field crews.
Exploring waterless biological digestion, smart IoT fill monitoring, and sustainable bio-based polymer manufacturing.
The transition away from chemical-heavy blue liquids toward natural enzymatic and biological treatment is accelerating. Next-generation camping urinals utilize bio-active cartridges containing specialized bacterial cultures that break down uric acid and organic compounds at the source, preventing scale build-up and eliminating pungent ammonia off-gassing.
Commercial outdoor event organizers and park managers are increasingly adopting smart portable units equipped with non-contact ultrasonic liquid level sensors. Connected via low-power NB-IoT or LoRaWAN networks, these devices transmit real-time fill-level telemetry to centralized logistics dashboards, optimizing pump-out routing and reducing operational maintenance costs by up to 40%.
Environmental, Social, and Governance (ESG) mandates are driving top manufacturers to incorporate post-consumer recycled (PCR) resins and sugarcane-derived bio-polyethylene into unit manufacturing. Leading suppliers are offering 100% recyclable product architectures, aligning with global net-zero carbon targets and municipal green procurement guidelines.
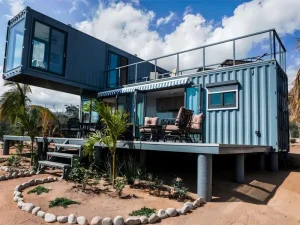
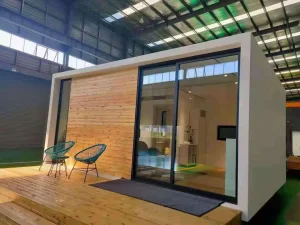
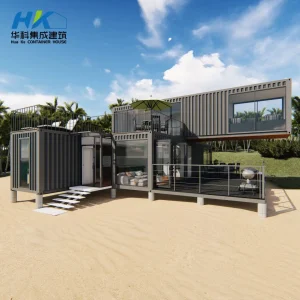
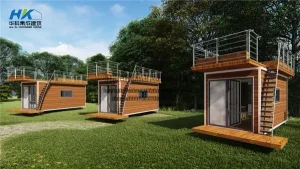
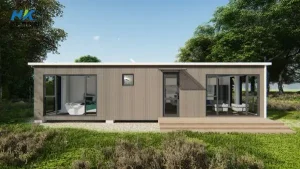
Rather than treating outdoor sanitation as isolated standalone accessories, modern architects are pairing portable urinals directly with modular container housing units, expandable light-steel villas, and pop-up commercial spaces, creating seamless, turn-key sanitary pods ready for immediate utility connection.
A standardized evaluation framework designed for procurement managers, import brokers, and commercial buyers.
Verify raw material specifications. Insist on virgin high-density polyethylene (HDPE) with UV-inhibitor packages (e.g., UV-8 rating minimum). Inspect wall thickness uniformity via ultrasonic testing to ensure structural integrity against high-impact loads and thermal expansion.
Examine the mechanical design of internal check valves. Continuous-duty silicone duckbill valves or magnetic flapper mechanisms are vastly superior to simple gravity flaps, which frequently fail when tilted or exposed to wind currents.
Evaluate unit nesting performance. High-efficiency suppliers design product geometry specifically so that nested components maximize volumetric fill within standard 40-foot High Cube (HC) shipping containers, drastically lowering ocean freight cost-per-unit.
Comprehensive answers regarding material specs, shipping logistics, customization options, and sanitation maintenance.
Tier-1 manufacturers primarily utilize UV-stabilized High-Density Polyethylene (HDPE) and high-impact Polypropylene (PP). HDPE is preferred for main holding tanks and structural walls due to its exceptional strength-to-weight ratio, high chemical resistance against acidic waste and harsh cleaning solvents, and superior performance in sub-zero or high-temperature environments. It resists cracking and won't absorb residual odors over extended service lifespans.
Waterless camping urinals prevent odor migration using a combination of mechanical and biological barriers. Mechanically, they incorporate one-way silicone duckbill valves, liquid-seal cartridges, or spring-loaded magnetic sealers that allow fluid to enter the holding reservoir while instantly snapping shut to block gas backflow. Biologically, enzymatic cleaning blocks or microbial dosing tablets are placed within the funnel trap to break down urea into odorless compounds before off-gassing occurs.
Yes. Many global resort developers and site contractors pair individual portable urinals or standalone mobile sanitation units directly with 20ft/40ft prefabricated container houses, expandable tiny homes, and modular flat-pack camp offices. Plumbing connections can be pre-configured with standardized quick-connect couplings for greywater/blackwater tank integration or external septic system hookups.
Under heavy commercial use (such as in mining camps, outdoor events, or public park installations), an industrial-grade HDPE portable urinal engineered with UV-inhibitors typically has a service life of 8 to 12+ years. Replacing wearing components—such as silicone seals, rubber gaskets, or chemical dispensers—every 12–24 months ensures long-term operational performance.
Top Chinese manufacturers optimize packaging using computer-modeled nesting techniques. Funnels, pipes, base tanks, and structural panels are designed to stack tightly within one another. Knocked-Down (KD) flat-pack packaging allows up to 300% more units to fit into a single 40ft High Cube container compared to fully assembled units, significantly reducing ocean freight freight cost-per-unit for international importers.
International buyers should look for ISO 9001 (Quality Management System) and ISO 14001 (Environmental Management) certifications. For product-specific compliance, CE certification, REACH compliance (verifying chemical safety of plasticizers and polymers), and ROHS compliance (for models with solar LED or electronic sensor components) ensure smooth customs clearance and regulatory compliance in European, North American, and Australian markets.
Browse additional custom modular homes, expandable container solutions, site office accommodations, and fast-install prefab structures.
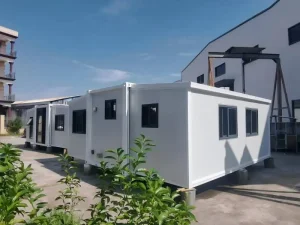
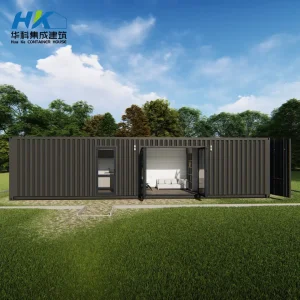
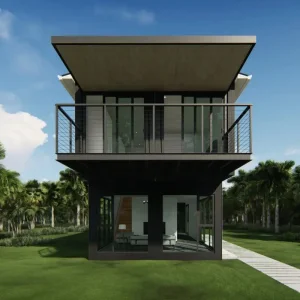
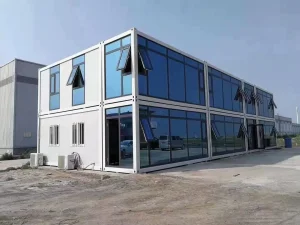
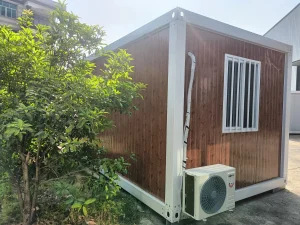
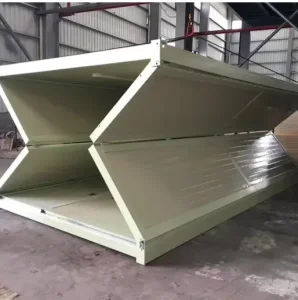
Whether you require OEM production runs of portable camping urinals, custom sanitation blocks, or complete modular container housing systems, our engineering team is ready to deliver tailored B2B solutions with global factory-direct efficiency.